HOW COMPRESSORS ARE USED IN PLASTICS & PET BLOW MOULDING
Continuous duty screw compressors coupled with high-pressure booster units for PET stretch blow moulding, injection moulding robotics, and scrap conveying.
The Critical Role of Compressed Air in Plastics & PET Blow Moulding
In plastics and packaging manufacturing, compressed air operates in two distinct pressure regimes. At low-to-medium pressure (7-8 Bar), rotary screw compressors drive high-speed Cartesian and 6-axis demoulding robots that enter injection mould cores during the 0.5-second mold open window to extract molded components, parts runners, and caps. At high pressure (25 to 35 Bar), a primary screw compressor feeds a booster compressor to stretch-blow heated PET preforms against water-cooled bottle mold cavities, forming transparent water, soda, and edible oil bottles at rates exceeding 30,000 bottles per hour.
Key Plant Machinery & Pneumatic Operations Powered:
Recommended Sarv Jagat Machinery Package
Sarv Jagat SJ RV50 Primary Screw + High Pressure Reciprocating Booster 30-Bar Package
Turnkey skid-mounted package with multi-stage high-efficiency coalescing filters, dual micro-porous pre-filters, and automatic zero-air-loss moisture drains.
STEP-BY-STEP PROCESS WORKFLOWS IN PLASTICS & PET BLOW MOULDING
Detailed examination of where and how compressed air powers each critical stage of the production floor, from raw material handling to final quality testing.
PET Preform Stretch Blow Moulding (High Pressure)
Primary air stretches the heated preform rod, followed by a 25-35 Bar high-pressure air blast that forces the hot polymer into intricate bottle mould details.
High-Speed Robot Demoulding & Parts Ejection
Pneumatic servo robot arms reach between mould platens to vacuum-grip and extract molded caps, automotive bumpers, or medical syringes.
Plastic Granule Vacuum Hopper Loading
Venturi air loaders convey virgin and regrind plastic polymer pellets from silos into drying hoppers and injection barrel throats.
ISO 8573-1 Air Purity Specification for Plastics & PET Blow Moulding
Plant air must adhere strictly to international purity thresholds to prevent expensive batch rejections, cylinder corrosion, and valve sticking.
Dual high-porosity sub-micron pre-filters eliminate microscopic dust particles, keeping pneumatic solenoids and servo valves operating with zero friction.
Guarantees no liquid water condensation inside the air network, preventing line rusting, painting blisters, and ice formation in refrigerated sections.
Multi-stage coalescing filtration and activated carbon towers ensure clean, vapor-free discharge compliant with strictest hygiene standards.
WHY ROTARY SCREW TECHNOLOGY IS ESSENTIAL IN PLASTICS & PET BLOW MOULDING
Discover why leading industrial facilities replace legacy reciprocating pistons with Sarv Jagat continuous-duty rotary screw compressors.
Engineering Advantage #1
High-pressure screw + booster tandem configuration saves massive energy over standalone 30-bar multi-stage pistons.
Engineering Advantage #2
Continuous air delivery prevents wall-thickness variation across PET stretch-blow cavities.
Engineering Advantage #3
Food-grade lubricant compliance ensures zero chemical taste or odor in bottled drinking water.
RECOMMENDED COMPRESSOR MODELS FOR PLASTICS & PET BLOW MOULDING
Click on any model below to view full engineering specifications, CAD dimensions, and air consumption sizing.
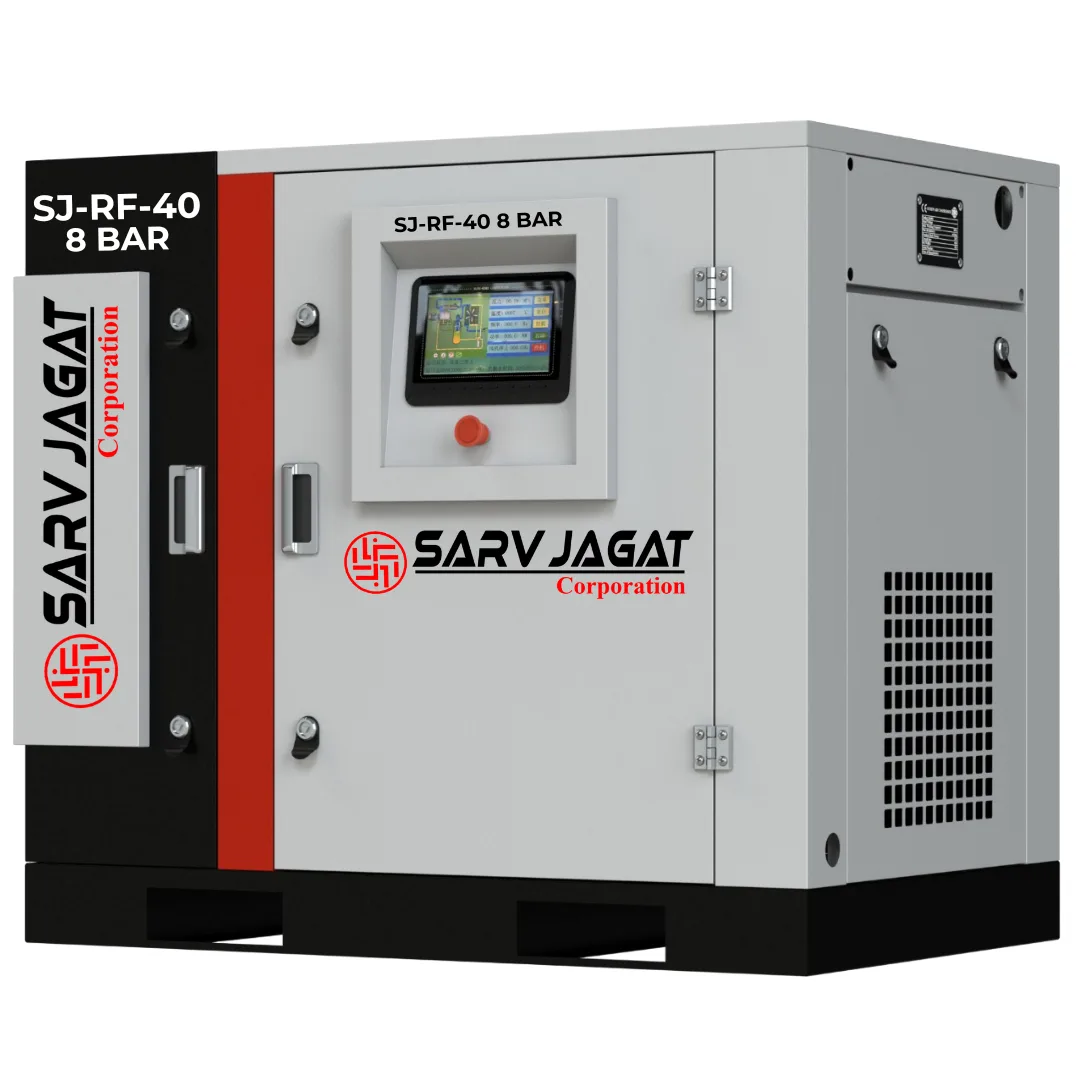
40 HP 8 Bar SJ Fixed Speed Screw Air Compressor
TECHNICAL FAQS: PLASTICS & PET BLOW MOULDING
Frequently encountered questions regarding air purity, pressure stability, and compressor sizing for this sector.
Q1:What is air recovery in PET blow moulding?
After a bottle is blown at 30 Bar, modern blow moulders exhaust the high-pressure air through an air-recovery circuit back into the plant 7-8 Bar line, saving up to 40% of factory pneumatic electricity.
Other Industries Powered by Sarv Jagat
Need Turnkey Engineering for Your Plastics & PET Blow Moulding Facility?
Our engineering team conducts free air audits, calculates pressure-drop curves, and recommends custom dual-voltage (380V/415V/460V, 50/60Hz) packages ready for containerized sea shipment worldwide.